How to Laser Cut Copper and Other Reflective Metals
From: 本站 Date: 03rd September 2021 Author: shengangtong Views: 4410
Laser cutting of mild steel and stainless steel has a long history and has been one of the primary applications for CO2 lasers. However CO2 lasers have not traditionally offered a good solution for cutting highly reflective materials.
Fiber lasers have an emission wavelength of around 1.07 µm, compared to 10.6 µm for traditional CO2 alternatives.
Not only is the 1.07 µm laser light reflected less, and therefore
absorbed more easily, but the shorter wavelength can be focused into a
spot that is around 1/10th of the diameter of a CO2 beam.
This provides a dramatically higher power density, making metal
penetration easier. At such high power density levels, metals such as
copper and brass quickly go through a phase change into molten state,
therefore the laser beam rapidly overcomes the reflectivity barrier of
such metals to initiate an efficient cutting process. Cutting such
metals have shown to be challenging using CO2 lasers or near lasers that have low peak power.
Why is laser cutting brass and copper so challenging?
Their low absorption of infrared laser light makes these metals challenging to cut.
Copper and brass (copper-zinc alloy) are good reflectors (and therefore poor absorbers) of the infrared (IR) laser light, especially in their solid state.
Pure copper reflects > 95% of near-IR radiation (~ 1 µm wavelength) in its solid state.
The reflectivity of copper and other reflective metals decrease when the metal warms up, and drops sharply once the material melts (e.g. down to <70% for copper in its molten state) as seen in figure below. These metals absorb significantly more laser energy in molten state.
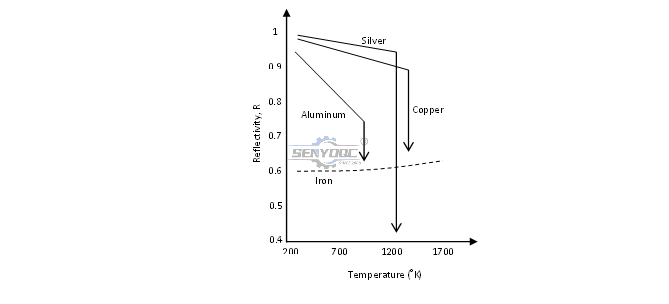
Common problems when laser cutting reflective metals.
When choosing optimized laser, optics, and cutting process, a laser beam
quickly melts the surface of reflective materials to then interact with
the more absorptive molten metal and initiate an efficient, stable
cutting process. Wrong choice of laser/optical setup, or using
non-optimal process parameters can result in excessive dwelling of the
laser with the solid metal, and therefore excessive amount of
back-reflected light. Too much reflection in turn results in the
inefficiency of cutting process and potential damage to optics.
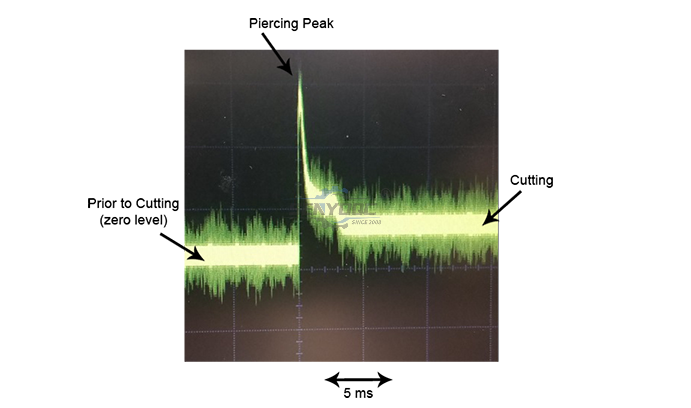
The critical stage in cutting reflective metal is the beginning of the
process, especially the piercing stage when the laser interacts with
solid metal. After the cut is established, laser beam mostly interacts
with the molten material.
What are the important factors in successful fiber laser cutting of copper and brass?
The following process parameters are relevant for piercing and cutting copper and brass with fiber lasers:
Cut Speed
Back off from the maximum feed rate the process can support by about 10 – 15% to avoid any risk that the cut will extinguish, thereby applying high levels of beam energy to a material in its most reflective state. If in doubt, start at a slower rate than you know the process can support. Allow sufficient dwell time to ensure pierce hole is through before moving the beam to start the cut.
Focus Position
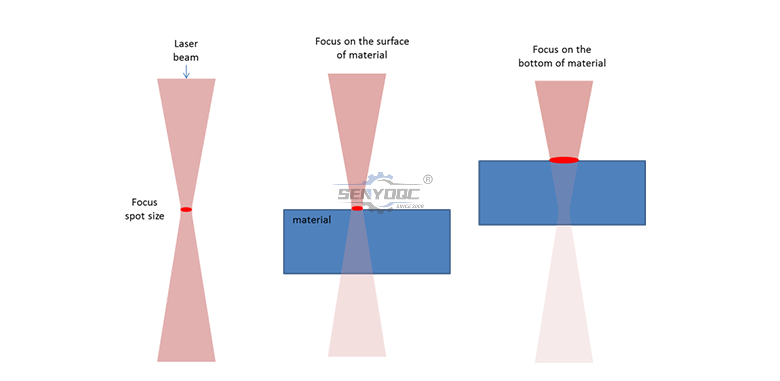
For both piercing and cutting, set the focus position as close to the top surface as the cut quality allows. This minimizes the amount of surface material that interacts with the beam at the beginning of the process, thereby maximizing the power density of the beam, which leads to quicker melting.
Power Setting
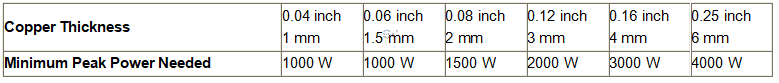
Using the maximum peak power available for the piercing and cutting
reduces the time in which the material is in its most reflective
condition. The chart above can be used as a conservative guide to start
the process development.
Cutting Gas
When piercing and cutting copper, using high-pressure oxygen (100-300 psi depending on the thickness) is typically used as the cutting gas to increase the process reliability. When oxygen is used, the formation of copper oxide on the surface reduces the reflectivity. For brass, nitrogen cutting gas works fine.


• Previous: Precision Cutting Stents with Fiber Lasers
• Next: Fiber Laser Cutting vs. Traditional Sheet Metal Cutting Techniques
Mini Desktop CNC Router for Gifts Making Small Business
Best Granite marble manual polishing machine For Sale
Stone Processing CNC Equipment Automatic Tool Changer CNC Quartz Stone Machining
3020 40W Mini CO2 Laser Engraving Cutting Machine
New Design Mini Stone CNC Machine for Marble, Granite and Quartz
Portable CNC Flame Cutting Machine with Plasma Torch for Sale
High-Precision Mini Hobby CNC Plasma Cutting Machine for Metal
Mini CNC Plasma Cutter With Rotary
4 Axis 1325 Sculpture Machine Cnc Carving Marble Granite Stone Cnc Router
Z Height 1000MM 4-AXIS Stone Engraving CNC Machine Heavy-duty Stone CNC Machine Stone Relief Carving CNC For Sale
4030 portable mini co2 laser carving and desktop rubber stamp laser engraving machine
Stone CNC Router For Kitchen sink tile carving and cutting Marble, Granite and Quartz
Robust CNC Plasma Cutting Machines with Flame Cut Head for Heavy-Duty Industrial Use
Small Portable CO₂ Laser Cutter Engraving for DIY & Business – Ideal for Wood, Acrylic, Leather
1325 3 Axis 4x8 CNC Stone Router for Sale
Mini CO2 Laser 5030 Cutting Engraving Machine For Sale
Portable CNC Plasma Flame Cutting Machine for Sale at Cost Price
Portable Cnc Plasma Oxyfuel Sheet Metal Cutting Machine for sale
CNC Plasma Cutters for Customized Metalwork –Rotary&Drilling Head
Small Table design 6040 Easy Move CO2 Hobby Laser Cutter Machine for Beginners
High-Efficiency 2 Heads CNC Machine for Aluminum Stone Marble Engraving & Cutting
Best CNC 2 Spindle 4-AXIS Stone Carving Machine High-precision Stone Carving Stone Countertop Fabrication
Top Rated 2x3 CO2 Hobby Laser Cutting Machine for Sale at Affordable Price
Best 4x8 CNC Plasma Cutter Table for Sale at Affordable Price
Entry Level CO2 Hobby Laser Cutter Machine for Beginners
Top CNC Plasma Cutters for Automotive, Aerospace, and Manufacturing Industries
Precision Stone Engraving Machines for Memorials & Signs
Portable Co2 9060 Laser Nonmetal Cutting Engraving Machine
1090 CO2 Laser Machine with Ruida Controller for Non-metal Glass Acrylic Engraving Cutting
Entry Level 9060 CO2 Hobby Laser Cutter Machine for Beginners
The Apprentice Maze Puzzle Box
Box laser cutting software share
laser marking and engraving for the jewelry industry
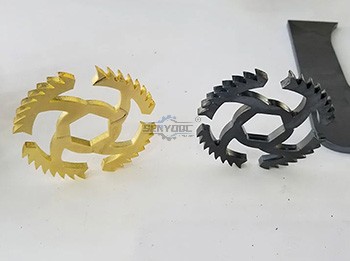
Copper cutting for fiber laser cutting machine
Aluminum Cutting for fiber laser cutting machine
CS Laser Cutting Factors that Affect the Process
Stainless steel Fiber Laser Cutting
2d&3d wood MDF carving and cutting
3D CNC Router for Stone Relief Carving Projects
Laser Cut Adjustable Table Lamp
CO2 Laser cutting Baby Birth Block
CO2 laser cutting and engraving for 6 Sided Box Puzzle
Co2 laser wood cut Illuminated Pattern Box
Engrave Round Parts With 50W Fiber Laser Marking Machine
CNC Plasma Cut Deer Head
Relief Map on a CNC Router
CNC Router Bar Stool
Wood Chair Made With CNC Router
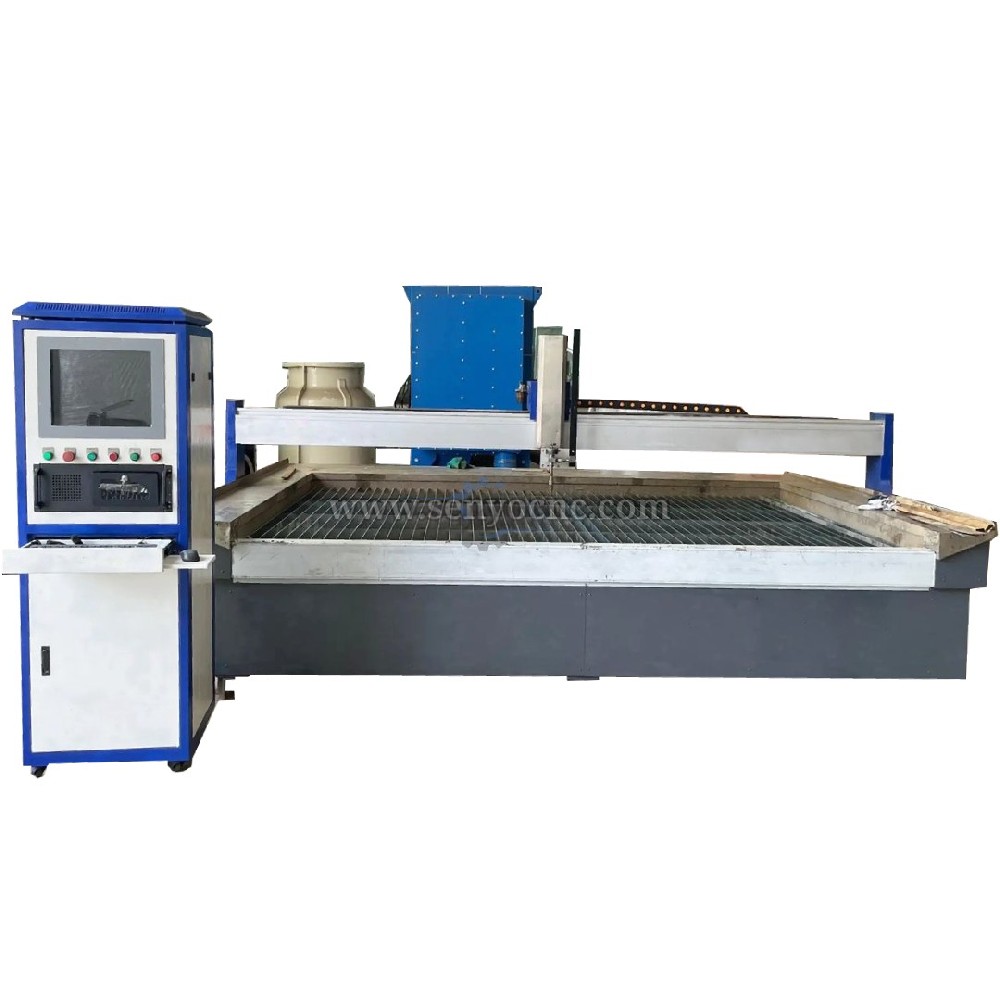
Competitive Price New Design Waterjet Machine 3 axis Cutting Machine
Typical industries that use waterjet technology
What main benefits to waterjet cutting ?
DTF Printer Machine Application
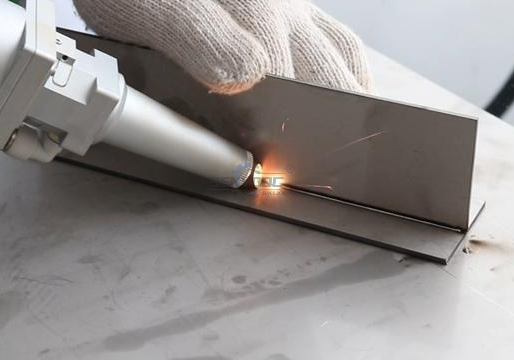
Typical fields of application
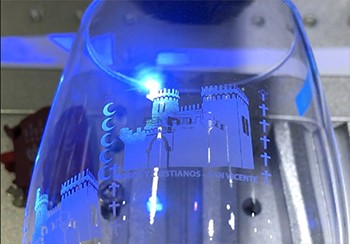
UV Laser Marking Machine For Glasses Engraving
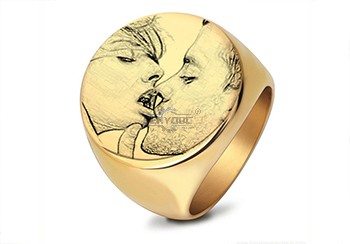
GOLD Engraving -Fiber laser marking work
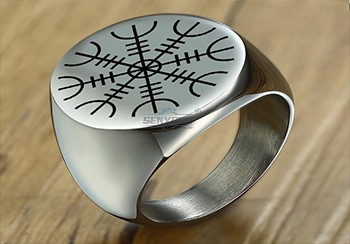
Sover Engraving -Fiber metal engraving and marking
3D Marking Logo deep engraving -Fiber marking machine
MOPA Fiber Laser Marking Machine Application and Samples
Fiber Laser Engraving and Marking Machine for Metalworking Projects
Stone shaft Rotary use engrave cnc router machine

Jacob from United States
I am a beginner at CNC, I’ve never used a CNC machine before and with in a day I was carving. An awesome machine for a beginner to learn as hobbyists. I used the manual and the help video. One hour to assemble and test, very friendly and easy to use. It’s a good buy for the money. I would definitely recommend this machine to someone getting into CNCs.
Weinstein from France
I've been using CNC plasma SYP2060-300A and I am very impressed with this unit.
This unit is of higher quality, made in China. Five stars all the way!
CO₂ Laser Cutting Machine SYJ1530 from 🇨🇦 Noah Campbell | Canada
We manufacture acrylic displays, signage, and decorative components for retail businesses.
Our work often involves cutting different shapes and engraving logos or lettering onto suitable acrylic sheets.
A CO₂ laser machine can support these applications when configured for the material and thickness involved.
It gives our team more flexibility when preparing custom designs and small production batches.
We appreciate being able to adjust cutting parameters to meet individual project requirements.
Multi-Spindle CNC Router from 🇦🇺 William Turner | Australia
We produce wooden furniture parts and decorative elements for local manufacturers.
Many orders contain repeated components that require similar machining operations。
Making a multi-spindle CNC router worth considering.
The machine provides flexibility when machining repeated designs with compatible tooling and suitable workpiece arrangements.
Matching the spindle configuration to the intended application is important, and this equipment offers another option for managing batch production
Marble CNC Engraving Machine SYS1560 from 🇫🇷 Pierre Martin | France
Our company works with marble for interior decoration, including engraved panels, customized signs, and ornamental stone products.
We wanted to introduce more digital processing into our workshop while retaining our existing stoneworking methods.
CNC engraving gives us flexibility when preparing designs with intricate lines and repeated decorative elements.
It is particularly useful for projects where customers require personalized designs reproduced according to specific layouts.
Fiber Laser Metal Cutting Machine from 🇹🇷 Ahmet Demir | Turkey
Our metalworking company processes sheet metal for industrial enclosures, brackets, and customized fabrication projects. We were looking for equipment that could handle digital cutting layouts and different component shapes. A fiber laser cutting machine can be suitable for this work when its power, working area, and material capacity match our requirements. The machine offers additional options for processing metal parts, and we emphasize correct setup and operator training.
SYM1325 Wood CNC Router from 🇺🇸 Michael Anderson | United States
We use this CNC router for cutting plywood, MDF, and solid wood panels in our furniture workshop.
The working area is suitable for standard-sized boards, reducing the need for repeated repositioning.
The machine supports our daily production tasks, including cutting cabinet components and engraving decorative patterns.
It has become a practical addition to our workshop, and we appreciate having
technical support available when questions arise.
SYJF50W Fiber Laser Marking Machine from 🇩🇪 Lukas Weber | Germany
Our company manufactures metal components that require identification numbers, logos, and product information.
A fiber laser marking machine provides a practical solution for marking compatible metal surfaces.
We use digital layouts to prepare different marking jobs, helping us organize production more systematically.
Choosing the correct parameters for each material is important, and the machine offers useful flexibility for product identification and customized branding.
SYM1530 CNC Router 4 Axis from 🇨🇱 Diego Morales — Chile
We use the machine for wooden prototypes, decorative parts and 3D models. The 4-axis capability allows us to create shapes that were difficult to produce before.
SYM1325 CNC ATC Router from 🇳🇱 Pieter Jansen — Netherlands
Our production includes cabinet doors, MDF panels and solid wood components. The automatic tool changer makes repeated production much more convenient.
 manager@senyocnc.com
 SENYOCNC
 +86 1525 3141 880
 +86 1525 3141 880
 2061579344
